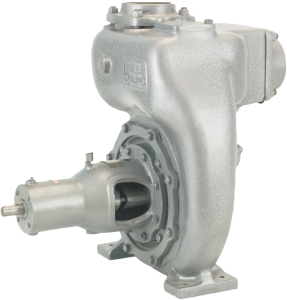
Industrial operations often involve transferring liquids, drilling fluids, and mixtures containing suspended solid particles. Such applications require strong and reliable pumping equipment that can work under demanding conditions. From construction and mining to drilling and manufacturing, businesses depend on suitable pumps to maintain smooth operations.
Different industries have different pumping requirements. Some need equipment for handling thick fluids, while others require pumps for high-pressure water circulation and large-volume fluid transfer. This is why choosing experienced Mud Pump Manufacturers is important for businesses looking for dependable industrial pumping solutions.
Understanding Mud Pumps and Their Industrial Applications
Mud pumps are specially designed pumping systems used to transfer drilling mud, slurry, and other fluids containing suspended particles. They are commonly used in drilling operations, mining, construction projects, and other heavy-duty industrial applications.
These pumps are designed according to the pressure, flow rate, fluid characteristics, and operating conditions of the application. Their construction and internal components help support fluid movement in demanding working environments.
Professional Mud Pump Manufacturers focus on developing equipment that meets different industrial requirements while providing reliable pumping performance.
Important Features of Mud Pumps
Heavy-Duty Construction: Mud pumps are designed with suitable materials and components to handle demanding industrial applications.
Slurry Handling: Depending on their design, they can transfer drilling fluids and liquids containing suspended solid particles.
High-Pressure Applications: Certain mud pump designs are suitable for operations requiring high discharge pressure.
Industrial Versatility: These pumps are used in drilling, mining, construction, and specialised fluid-transfer applications.
Before purchasing a mud pump, businesses should check the liquid properties, solid content, required flow rate, operating pressure, and maintenance requirements. Reliable Mud Pump Manufacturers can help buyers select suitable equipment for their applications.
Why Choose Boiler Feed Pump Manufacturers for Industrial Operations?
Boilers are widely used in power generation, manufacturing, chemical processing, and other industrial facilities. They require a continuous supply of water at a suitable pressure to maintain proper operation.
Boiler feed pumps are designed to transfer water into boilers against the pressure inside the boiler system. These pumps play an important role in maintaining a consistent water supply and supporting efficient boiler operations.
Experienced Boiler Feed Pump Manufacturers focus on producing equipment that can meet the pressure, temperature, and flow requirements of different boiler systems.
Key Benefits of Boiler Feed Pumps
High-Pressure Performance: These pumps are designed to deliver feedwater at the pressure required by the boiler system.
Reliable Water Supply: They help maintain a continuous supply of water during boiler operation.
Industrial Applications: Boiler feed pumps are commonly used in power plants, manufacturing facilities, refineries, and process industries.
Application-Specific Designs: Different pump configurations are available depending on boiler capacity, operating pressure, and water requirements.
When selecting a boiler feed pump, businesses should consider operating pressure, water temperature, flow capacity, pump efficiency, and material quality. Professional Boiler Feed Pump Manufacturers can guide buyers in choosing equipment suitable for their boiler systems.
Understanding Split Casing Pump Manufacturers and Their Applications
Industries that require large quantities of water often need pumping equipment with high-flow capabilities. Split casing pumps are commonly used in water supply, irrigation, power generation, and industrial circulation systems.
These pumps feature a horizontally split casing arrangement that provides convenient access to internal components during inspection and maintenance. This design makes them suitable for installations where regular servicing and reliable water movement are important.
Reliable Split Casing Pump Manufacturers develop equipment according to different flow requirements, operating conditions, and industrial applications.
Important Features of Split Casing Pumps
High Flow Capacity: These pumps are suitable for applications requiring the movement of large volumes of water.
Convenient Maintenance: The split casing design allows easier access to internal pump components.
Strong Construction: Proper material selection and engineering support dependable performance in demanding applications.
Wide Applications: These pumps are used in irrigation, water supply, industrial cooling, and power plant operations.
Before purchasing, buyers should compare flow rate, total head, efficiency, material compatibility, and installation requirements. Experienced Split Casing Pump Manufacturers can help businesses identify suitable pumping solutions.
How to Choose the Right Industrial Pump Manufacturer
Selecting a reliable manufacturer is an important step when purchasing industrial pumping equipment. Businesses should consider product quality, technical specifications, manufacturing experience, and customer support before making a decision.
Here are some important factors to consider:
Manufacturing Quality: Check the materials, construction, and overall pump design.
Technical Specifications: Compare flow rate, pressure, temperature limits, and application requirements.
Product Range: Explore different pump models to find suitable equipment for your industrial process.
Industry Experience: Consider the manufacturer’s experience in providing industrial pumping solutions.
Technical Support: Choose a manufacturer that offers product guidance and maintenance assistance.
Evaluating these factors can help businesses select suitable pumping equipment and support smooth industrial operations.
Why Choose JEE Pumps Limited?
When looking for dependable industrial pumping equipment, businesses should consider manufacturers that understand different fluid-handling requirements. JEE Pumps Limited offers industrial pumping solutions for various applications across different industries.
Selecting the right pump requires understanding the liquid properties, required flow rate, operating pressure, temperature, and installation conditions. These factors help determine the most suitable pump design for each application.
Whether a business requires equipment for drilling operations, boiler water supply, or high-volume water transfer, selecting the correct pump configuration is important for maintaining reliable performance.
JEE Pumps Limited is a manufacturer businesses can explore when looking for industrial pumping solutions. Buyers should review product specifications and discuss their application requirements to identify suitable equipment.
Conclusion
Choosing the right industrial pump is essential for maintaining efficient operations and reliable fluid transfer. Mud pumps are designed for drilling fluids and slurry applications, boiler feed pumps support high-pressure water supply to boilers, and split casing pumps are suitable for high-volume water transfer. Businesses should compare technical specifications, construction quality, material compatibility, and maintenance requirements before purchasing. JEE Pumps Limited is a manufacturer businesses can explore for dependable industrial pumping solutions.